Rotary screw vacuum pumps and screw compressors share the same core technology. As a result, the two share many similarities. But there are some differences.
And those differences can make a huge impact on industrial vacuum applications. And some of them might surprise you.
Let’s compare those similarities and differences.
Contrast No. 1. Precision
Precision is important in compressed air, mostly to conserve energy. But it’s even more important in vacuum technology, because it’s not about producing the deepest vacuum possible. It is about using a properly sized pump of the right technology to provide a stable, repeatable vacuum level, day in and day out, for a wide range of industrial vacuum applications, where precision is required.
A few examples:
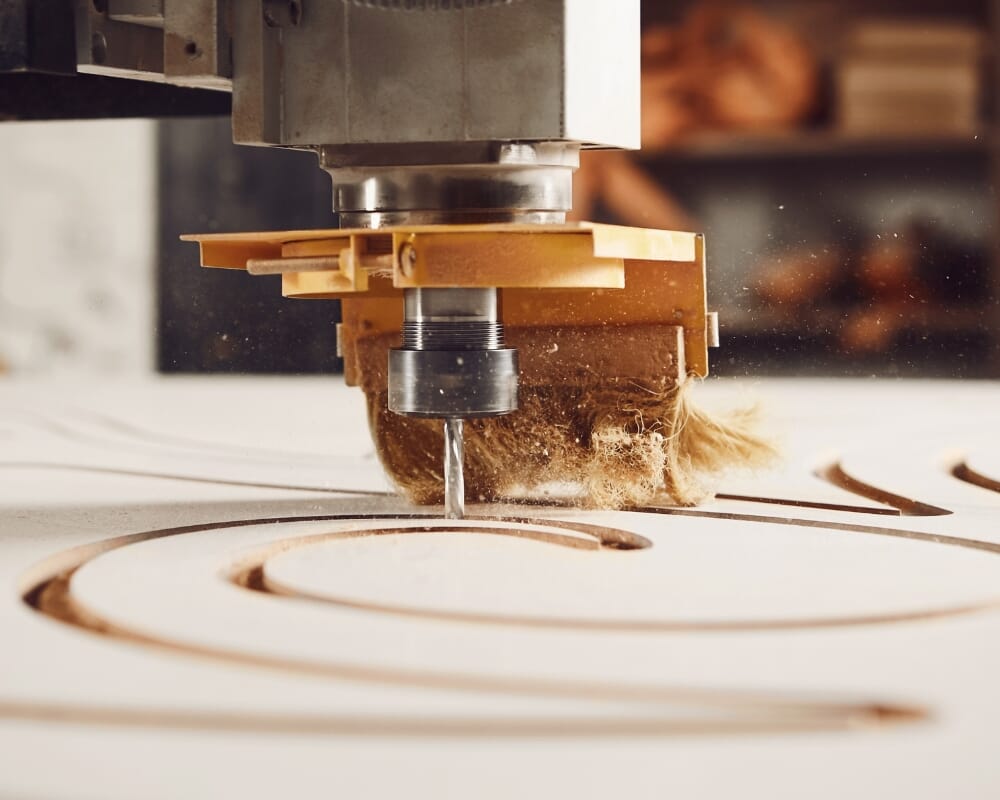
- Cabinet shops use vacuum technology to hold plywood sheets flat on a CNC router table so that the cutter can trace the pattern precisely. If it’s off even slightly, an entire sheet of plywood is scrap.
- Composite molding fabricators lay fiberglass or carbon fiber in a mold, bag it and use the vacuum to pull out air, pressing the laminate perfectly flat before injecting resin. The vacuum level must be stable to produce extremely thin, consistent parts.
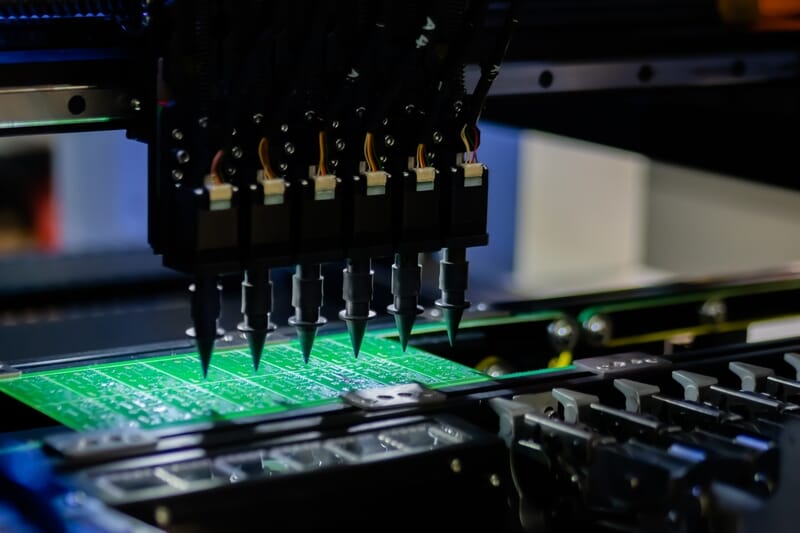
- Robotics and other low vacuum applications need repeatable vacuum levels to execute pick-and-place operations with pinpoint accuracy.
Contrast No. 2. Process
While you can’t ignore process in specifying an air compressor for a specific use, the application and setting are critical for vacuum technology. It drives equipment selection much more than it does in compressed air.
In fact, there are some situations in which the application dictates which vacuum technology can be used:
- Vapors recovered from a chemical plant would probably destroy an oil-flooded pump in a matter of hours. The plant should probably use a liquid-ring system instead.
- Applications generating heavy water vapor loads would probably be best served by a liquid ring pump. With an oil-flooded pump, vapors would condense at startup and shutdown, then mix with the fluid. And water spells trouble in most mechanical equipment.
Rotary screw vacuum pumps can handle vapor up to a point, but you should tailor the process around keeping the pump hot. You don’t want to turn the pump off, let it cool down and then start up again, because the water vapor will come into contact with the cold surfaces inside the pump and condense. Once again, that’s not good.
Contrast No. 3. Pressure Range and Performance Curves
An industrial air compressor increases atmospheric air to a substantially higher discharge pressure. For example, a compressor rated at 115 PSIG produces a pressure differential of approximately 8 bar.
A vacuum pump, on the other hand, works in the opposite direction, reducing the inlet pressure below atmospheric pressure. Because a perfect vacuum represents zero absolute pressure, the maximum theoretical pressure differential is one atmosphere—approximately 14.7 psi or 1 bar at sea level.
That narrower pressure differential does not make vacuum-pump selection simple. A pump’s available inlet flow changes with the vacuum level, so a capacity rating without its corresponding operating vacuum can be misleading. Nameplate capacity should never be compared directly with another pump’s performance at a specific vacuum level.
The correct approach is to establish the required ACFM at the system’s actual operating vacuum, then compare that operating point with the manufacturer’s published performance curves. This ensures the selected pump provides the required flow where the process actually operates—not merely at its maximum nameplate rating.
Kaishan covers the industrial rough-vacuum range with six KRSV models from 10 to 125 HP, providing capacities up to 3,505 CFM.

As a result, vacuum pumps have a much smaller capacity range, so Kaishan covers the full rough vacuum range with six different sizes, ranging from 10- to 125-HP units.
Contrast No. 4. Heat of Compression
As they generate such a significant pressure range, air compressors create a lot of heat, so they need large coolers to dissipate it. The 7- or 8-bar compression levels also concentrate moisture in the air, making condensation a constant concern.
With vacuum pumps, however, the pressure range is smaller. Vacuum pumps still require heat management, and condensable process vapor can be a major concern. Perhaps to a lesser extent per CFM than in compressors. But it is still a major concern and should be taken into account in the selection phase.
Contrast No. 5. Sizing
As we have pointed out many times in this space, sizing is extremely important for air compressors. Oversizing a rotary screw compressor, for instance, is the leading cause of rapid cycling, which causes maintenance nightmares, equipment failures and downtime.
Oversizing isn’t as much of an issue with vacuum pumps as it is with air compressors. A 50-HP pump running at 300-400 CFM is not going to consume significantly more power than a 30-HP pump. But that 50-HP unit has a much higher top end.
So, if we’re right on the borderline between two sizes, I generally recommend the larger model equipped with a variable-speed drive. Because, with a VSD, you can always turn it down. That always stumps air compressor pros, whose biggest fear is oversizing.
Contrast No. 6. Use of Variable-Frequency/Variable-Speed Drives
When you run an air compressor at a fraction of its full capacity, frequent stops and starts aren’t good for the pump, and you’ll start condensing a lot of water as the pump cools down when it’s not generating air.
As mentioned, water is much less of an issue with vacuum pumps. So turning a vacuum pump down to a lower pressure presents less risk of condensation.
Some rotary screw vacuum pumps equipped with a VFD can turn down to as low as 10%. With that kind of range and little threat of moisture accumulation, there’s very little penalty for oversizing VFD/VSD vacuum pumps.
Contrast No. 7. System Pressures
As in compressed air, most of these projects are about energy efficiency. So, you want to use the lowest vacuum level that reliably meets the process requirements:
- If you run too deep a vacuum, it’s like running a compressor at too high a pressure; you’re wasting energy.
- But if you run a vacuum that’s too shallow, you’ll experience product loss.
For many companies, it’s a balancing act, and the vacuum system must operate in a tight window.
I was at a plant recently where they used vacuum to remove air from aerosol cans. If they didn’t have enough vacuum, they couldn’t remove enough of the air and oxygen from the cans. But if they ran a vacuum too deep, it would collapse the can.
Another example is a bakery that is pulling loaves from pans using suction cups. Too little vacuum and the bread won’t come out of the pan. Too much, and the vacuum damages the top of the bread.
Contrast No. 8. Inlet Filtration
While inlet filtration is extremely important in compressed air, it’s mission-critical in vacuum. A vacuum, after all, draws in all the dust, dirt and vapors present in the workspace, and those contaminants must be removed before the air reaches the vacuum pump.
Inlet filtration is always required regardless of process or technology. If you suck up dirt and other material and don’t have an inlet filter, that’s not a warranty event. It’s an operational failure.
Without proper inlet filtration, vacuum pumps are at much higher risk of failure. You’ll shut down without proper filtration and proper filtration maintenance.
Contrast No. 9. Oil Sampling
Oil sampling is important in both technologies. We require customers to draw and analyze an oil sample every 2,000 hours to maintain warranty coverage on most of the oil-lubricated products we make—both air compressors and vacuum pumps.
With vacuum pumps, however, oil sampling is especially important. It may be the first indication that something’s wrong or something is changing in your process. In one food and beverage plant I visited, the company started using a citric acid powder that got into the air and changed the fluid’s pH. That could easily rust a pump’s internals.
As a result, in vacuum, oil sampling is important because we’re drawing in process materials and vapors, including harsh chemicals that can cause corrosion and premature wear if not monitored closely.
Contrast No. 10. Routine Maintenance
At the end of the day, our vacuum pumps are rotary screw pumps. They use the same technology as the other rotary screw pumps we make.
So, they require the same routine maintenance: changing lubricants, oil sampling and replacing separators and filters. All tailored to each specific process and fluid type.
And, of course, you’ll want to pay attention to the key warning signs:
- Longer evacuation times
- Unstable vacuum
- Increased temperature
- Increased power usage
- Frequent filter changes
Three Steps to Getting Vacuum Technology Right
1. Understand the Process
Some processes are incompatible with certain vacuum technologies, so you need to consult with an expert that understands the application, what the process air may contain, and the limitations of the technologies being considered.
2. Find Out What Pump Is Currently Being Used
You can’t just rely on nominal pump data tags to understand actual vacuum performance. You need to know the actual vacuum level the current pump is reaching, measured with a vacuum gauge, and not rely solely on the machine tags. With that information and the performance curves, you can calculate exactly how much flow (ACFM) you’re using.
3. Only Then, Pick the Pump
With the flow rate and the vacuum level, you can find the values on a selection chart and pick the pump you’ll need.
The best way to start? Get expert help.
Expert Help
Most vacuum pump manufacturers do not have local technicians or service centers. If you need service, you have few options besides sending a broken pump to an authorized service center.
The good news is that the same people who service Kaishan rotary screw compressors can also maintain and repair your rotary screw vacuum pump. You have fewer vendors and a dependable, one-stop resource you can count on when your equipment needs service. When they’re servicing your compressors, they can often address any vacuum issue during the same visit.
Many companies save significantly by using the same supplier for related vacuum and compressed air needs.
Kaishan USA works with a nationwide network of independent distributors because it’s the best way to ensure you get the expert guidance, faster response times and personalized support you need.
These factory-trained experts can provide on-site help and have staff skilled in advanced technology. They can service your vacuum or air compressor system without a problem.
With factory-trained technicians and a deep understanding of industrial vacuum applications, they help maximize efficiency and minimize downtime. So, when you buy through Kaishan, you’re getting more than a product—you’re getting a local partner who cares about your business and wants to see it succeed.
Kaishan’s KRSV: Plant Engineering’s 2025 Product of the Year
Kaishan’s KRSV rotary screw vacuum pump is the ideal solution for a wide range of facilities, providing industry-leading efficiency and rugged reliability while reducing maintenance and electrical costs.
In fact, Plant Engineering magazine named it 2025 Product of the Year.
It is the only industrial vacuum pump on the market that integrates a VSD and a variable-discharge port. As a result, the KRSV delivers the most CFM per horsepower at every vacuum level, helping you keep electricity consumption to a minimum.
The combination of the variable-discharge port and the external oil pump lets you ramp up faster, significantly boosting productivity. In tests, the KRSV drew a 500-gallon tank down to vacuum 28% faster than a pump with only a VSD.
With both VSD capability and a variable-discharge port as standard features, Kaishan’s KRSV gives you an unequaled operational range (with turndown capabilities up to 90% of maximum).

The KRSV rotary screw vacuum pump delivers the most CFM per horsepower at every vacuum level.
The KRSV is ideal for the bread-and-butter rough vacuum range that serves many industrial applications. Typical uses include CNC woodworking, packaging, pharmaceutical production and composite molding where vacuum precision directly impacts product quality and waste reduction.
Key Takeaways
- Precision in a vacuum system means using a properly sized pump with the right technology to deliver a stable, repeatable vacuum level, day in and day out.
- Process drives equipment selection much more in vacuum than it does in compressed air.
- Oversizing isn’t as much of an issue with vacuum pumps as it is with air compressors. Because of the larger turndown range in a VFD/VSD pump, there’s almost no penalty for oversizing a vacuum pump.
- A vacuum pump always requires inlet filtration, regardless of process or technology.
- Oil sampling may be the first indication that something’s wrong with a vacuum pump or that something is changing in your process.
The Help You Need, When and Where You Need It
Kaishan USA works with a nationwide network of independent distributors, who can provide on-site help and consultation as needed.
We partner with independent, local distributors because it’s the best way to make sure you get the right system, reliable service and quick access to parts when you need them most.
With factory-trained technicians and a deep understanding of industrial applications, they help maximize efficiency and minimize downtime.
So, when you buy through Kaishan, you’re getting more than a product—you’re getting a local partner who cares about your business and wants to see it succeed. Contact us today.
Further Reading
“The Top 10 Vacuum Pump PITAs for Woodworkers (and how to fix them).” We review ten real-life pain points that apply to almost any rough vacuum application.
Frequently Asked Questions
Listen to the Podcast Version
Comparing and Contrasting Vacuum Pumps and Air Compressors
Welcome to the Big Dog Podcast. I'm Jason Reed, and this is where we talk compressed air without the fluff.And I'm Lisa Saunders. Today we're comparing and contrasting vacuum pumps and air compressors. Here's what makes it interesting. Rotary screw vacuum pumps and rotary screw air compressors share the same core technology, interlocking helical rotors turning inside a casing. So you'd think anyone who knows compressors could walk up to a vacuum pump and be right at home.
On maintenance, they mostly would be. Fluid changes, separator elements, oil sampling, filters, all the same routine, tailored to the process and the fluid. But the physics run in opposite directions, and that changes how you have to think. A compressor takes atmospheric air and pushes it up. A unit rated at 115 P.S.I.G. builds a differential of roughly 8 bar. A vacuum pump pulls the inlet below atmospheric. Perfect vacuum is zero absolute pressure, so the most differential you can ever get is one atmosphere. That's about 14.7 psi, or 1 bar, at sea level.
So eight bar of work on one side and one bar on the other. Does the smaller number make selection easier?
It doesn't, and that surprises people. A vacuum pump's inlet flow changes with the vacuum level. So a capacity number with no vacuum level attached can mislead you. You can't set one pump's nameplate beside another pump's performance at a specific vacuum and call it a comparison. The right way is to measure the actual vacuum at the process with a gauge, work out the ACFM you need at that level, then plot that operating point on the published performance curves.
That's why replacing a pump with the same horsepower is a trap. The motor rating on the tag says very little about what the process needs.
Exactly. And it connects to the idea of precision. People hear vacuum and picture the deepest vacuum possible. In industrial work, that's usually not the goal.
Right. Say a process needs 24 inches of mercury. It doesn't need a pump that occasionally touches 29.9. It needs one that holds 24 every cycle and every shift, without drift.
A cabinet shop shows why. Vacuum holds a plywood sheet flat on a CNC router table so the cutter can trace the pattern. If the hold is off even slightly, the whole sheet is scrap. Composite fabricators lay fiberglass or carbon fiber in a mold, bag it, and pull the air out to press the laminate flat before injecting resin. The vacuum has to be stable to get thin, consistent parts. And robotic pick and place needs repeatable vacuum to land with pinpoint accuracy.
Then there's the window problem, where both too little and too much cost you. Picture a plant evacuating aerosol cans. If the vacuum is too weak, you leave air and oxygen in the can. Run it too deep and you collapse the can. Or a bakery using suction cups to lift loaves out of pans. Too little vacuum and the bread stays put. Too much and you damage the top of the loaf.
It's the same logic as compressor pressure. Run too deep and you waste energy, like a compressor set too high. Run too shallow and you lose product. You want the lowest vacuum level that reliably meets the process.
Sizing, Vapors and Keeping Vacuum Healthy
Now let's get to the one that stumps compressor people. Sizing.In compressed air, oversizing a rotary screw compressor is the leading cause of rapid cycling, and that brings maintenance headaches, failures and downtime. Run one lightly loaded and it cools off, then you start condensing water. Vacuum is different. Water is much less of an issue, and some rotary screw vacuum pumps with a variable frequency drive can turn down to as low as 10%. A 50 horsepower pump running at 300 to 400 CFM won't consume significantly more power than a 30 horsepower pump. But the larger one has a much higher top end.
So if you're right on the borderline between two sizes?
Go with the larger model and a variable speed drive, because you can always turn it down. Compressor pros hate hearing that, since oversizing is their biggest fear.
But vapor can still hurt you. Some processes decide the technology before anything else. If vapors recovered from a chemical plant hit an oil flooded pump, they'd probably destroy it in hours. A liquid ring system is probably the better fit. Heavy water vapor loads usually point the same way.
Because with an oil flooded pump, vapors can condense at startup and shutdown and mix into the fluid, and water spells trouble in most mechanical equipment. Rotary screw vacuum pumps can handle vapor up to a point. But you build the process around keeping the pump hot. Don't shut it off, let it cool, and start it again, because vapor meets those cold internal surfaces and condenses.
And a compressor draws in the air around it, while a vacuum pump pulls in the process itself. Sawdust, dirt, vapors, whatever is in that workspace.
Which is why inlet filtration is mission critical. It's always required, regardless of process or technology. If you suck up debris with no inlet filter, that isn't a warranty event. It's an operational failure.
Oil sampling matters too. Every 2,000 hours is the interval on most oil lubricated compressors and vacuum pumps. But in vacuum it can be your first warning that the process changed. Think of a food and beverage plant that started using citric acid powder. It got into the air and changed the fluid's pH, and that could easily rust a pump's internals.
The oil reflects whatever the process gives off. A change in the oil often signals a change in the process. And watch for the physical warning signs: longer evacuation times, unstable vacuum, higher temperature, more power draw, and frequent filter changes, especially on exhaust oil mist eliminators.
One practical note. Most vacuum pump manufacturers don't have local technicians, so a broken pump may mean shipping it to a service center. But since the technology is shared, technicians who work on rotary screw air compressors can often maintain rotary screw vacuum pumps too, sometimes in the same visit.
So the order is simple. Understand the process, measure what the current pump actually delivers, then pick the pump from the curves.
That's our time. Thanks for tuning in to the Big Dog Podcast. I'm Lisa Saunders.
And I'm Jason Reed. Thanks for listening, and we'll catch you next time.